“Whatever you do, work at it with all your heart, as working for the Lord, not for human masters.” Colossians 3:23 (NIV)

Category: Bright IA

  • Modbus TCP with no middleman on an Allen-Bradley PLC

    Modbus TCP with no middleman on an Allen-Bradley PLC

    Hello, automation fam,

    It took quite a bit 😅 to come back and write to our blog, but here we are with another real application and case study.

    As our logo states “simplified automation”, for us is not just a marketing slogan but instead is our belief, keep it simple, keep it smooth.

    This is the case for this application where we were tasked to make talk a ControlLogix with a pH controller.

    As a lot of you know, the most famous and used communication protocol is Modbus, and most of these specialty devices can communicate over Modbus.

    But what we were thought to always do, in the case we had to pass information from/to Allen Bradley and other devices via Modbus TCP, was to purchase a piece of equipment such as Redlion or Anybus and use it as a protocol converter.

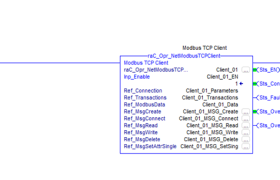
    But a few years ago, Rockwell released this add-on instruction that allows implementing the Modbus protocol to the Ethernet/IP communication. While the first release was a little bit tricky, the latest has been dramatically improved, this resulted in the fastest solution deployment.


    intelligent automation blog
    Screenshot of the add-ons instruction

    After watching one of the Tim Wilborne from TW controls videos, an opportunity just came to happen to use the AOI, and we did it successfully.

    As always, you must deal with offsets, pulling rates, and end devices setup, but other than that, we were able to use both read and write commands and control the device (in our case a Walchem W600 pH controller) from the HMI.


    Some setups need to happen, to be able to make this work:

    1. Make sure to place your Modbus add-ons on a subroutine that run at 20 ms periodically

    2 – messages can overlap with each other, while we did not experience any loss of data, is always a good practice to set different pulling rates, play with the numbers until the “overlap” bit will go away.

    3 – Put the tags you are using to communicate with the HMI on a lower scan routine, this is another good practice, since we are using fast scanning, we want just the Modbus communication to sit in there, while the tags and other manipulation (i.e., 2 words to float), will stay on a slower scanning task.

    4 – If You can’t connect with your setup at the first attempt, it’s always good to have in your toolbox software such as Modbus poll and verify that the famous port 502 is enabled via telnet.

    Something that we did not mention earlier is that the AOI has the server and the client version, in our scenario we used the client mode, but we do think it would make too much difference to integrate by using the server function.

    In conclusion, we are pleased to have found this awesome solution, especially with so many issues we are experiencing with the supply chain, and how difficult is to find devices, this is a great and cost-effective solution to get the customer up and running in little time. Who isn’t for a simplified and quick solution?

    As always, we are here to help, if you need any support on this or other related matters, contact us, or drop a comment below, we’d like to talk about this stuff all day long.

    Until next time,

    Have Fun!

    P.S. Committed to making your life easier.

  • How to overcome the current supply-chain situation

    How to overcome the current supply-chain situation

    First of all, do not Panic! But, where to start?

    My name is Davide, I am the Chief Automation helper at Bright IIOT, and today we are going to discuss current and hot topics. Share with me 5 minutes of your time.

    The Factory’s maintenance, operation management are recently struggling with the following obstacles: 

    • Shortage of workforce 
    • Equipment renovation 
    • Demand and supply = throughput 

    But the question is, where to start or how to overcome at least one of the obstacles? 

    Shortage of Workforce

    We all know that after these struggling times, it’s difficult to find and hire talents or attract them to come back to the market. 

    Let’s pretend that these people will work in your production lines, processes that are already in your plant/plants, but in this case, they are not available or you could not find any candidate willing to work with you. 

    intelligent automation blog

    The first question to ask is: in your existing process, which involves automation and automated equipment, is there anything that could be IMPROVED, manipulated, updated that could remove some manual operation or intervention? 

    Think about repetitive operations such as adjusting parameters each time some events happen, moving material from point A to point B, writing down reports, or needing to historize and mine data? Calculate how efficient is your process. 

    All of these things and more can be automated and let the workforce, you were able to keep with you, focus on dynamic tasks that really require human intervention. This is the aid of automation. 

    Machine and equipment renovation

    I am going to change the tone here as I am pretty sure you have machines and equipment that you give constant maintenance and cleaning to keep them ready and precise for the next task. 

    The same applies to the automation that lets these machines run and operate in everyday tasks. 

    The automation devices will deteriorate over time and they are not reliable anymore, especially old PLC with EEPROM memories. 

    But more than that, it also depends on where these devices operate, is the control panel installed in a too hot, too cold, too acid environment? 

    Also, do you have backup copies of your source codes, spare batteries for the memory, spare I/O cards, power supplies, etc.? 

    Do you have old relay logic panels that you would like to improve and maybe modify the logic to accommodate another product, another function, etc.? 

    In other words, can you afford to stay down for more than 30 minutes in your plant? If the answer is NO, then you should lay down a maintenance plan and eventually retrofit your automation and improve exponentially the reliability. 

    LET’S DISCUSS RIGHT NOW 

    Last but not least is demand VS Supply 

    As we are well known, the demand surged in the last months and no sight is going to normalize anytime soon. 

    My question is, what actions are you taking to keep up with these orders requests? 

    Is automation the right answer to the problem? 

    Probably yes, even though our industry is affected by the supply chain crisis, we can always utilize the hardware that is available in the market by selecting and mixing several manufacturers or going to find refurbished parts. Either way is possible. 

    With that being said, is the duty of the end-user to identify his/her system bottlenecks and unclog them with targeted actions which could intervene in the existing systems and add a couple of sensors or cameras or robot arms or could automate a line. The sky is the limit, 

    But more importantly, to be able to track the changes applied to the processes, the end-user should implement a metric system that will monitor and report each process, each machine, and also the overall plant efficiency. 

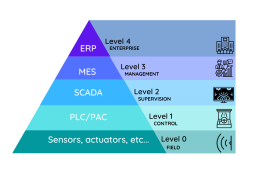
    This exercise is not only beneficial for high-rank corporate people but For the plant floor personnel as well, where they can constantly and real-time monitor the performance and reliability of every single machine. The OEE (Overall Equipment Effectiveness) and MES (Machine Execution System) are the two methods widely used in our industry. 

    DO YOU WANT TO LEARN MORE? Click HERE 

    Conclusions

    In conclusion, as we said earlier, the sky is the limit, but you need to start somewhere if you want to keep with the competitors and stay on the edge of the innovation. 

    The technologies are moving faster than ever, and if you are a company that wants to stay in the game for a long time and want to be profitable and pay and treat your employees well, then you cannot afford not to take massive actions. 

    The digital transformation is here, and few companies are starting to realize that is time to make the next move, don’t be the majority that is sitting there and think that things will stay the same as 20 years ago. 

    If you are interested in talking FREELY about these topics, contact me, I would love to hear your feedback. 

    Thank you, 

    Davide @ Bright IIOT

    “Changing the automation industry one signal at the time.”

    Romans 1:16

    #automation #scada #mes #oee #retrofit #industrialautomation #manufacturing #oem #supplychain #industry4 #iiot #industry40 #controls #reports #programming #efficiency 

  • Welcome to our 4.0 Blog Page!

    Welcome to our 4.0 Blog Page!

    Get the Latest News on Industry 4.0.

    Interested in the world of digital transformation? Ready to discover how Industry 4.0 is taking the globe by storm? Luckily for you, you’re in the right place. In this blog, you can expect to discover all of the latest news, updates, and thought-pieces from Bright IIoT.

    Stay tuned and get in touch if you have any questions about our offering.

servicefree servicsdfve